Platt / Retail store fixtures
Built to the pitch your system already uses.
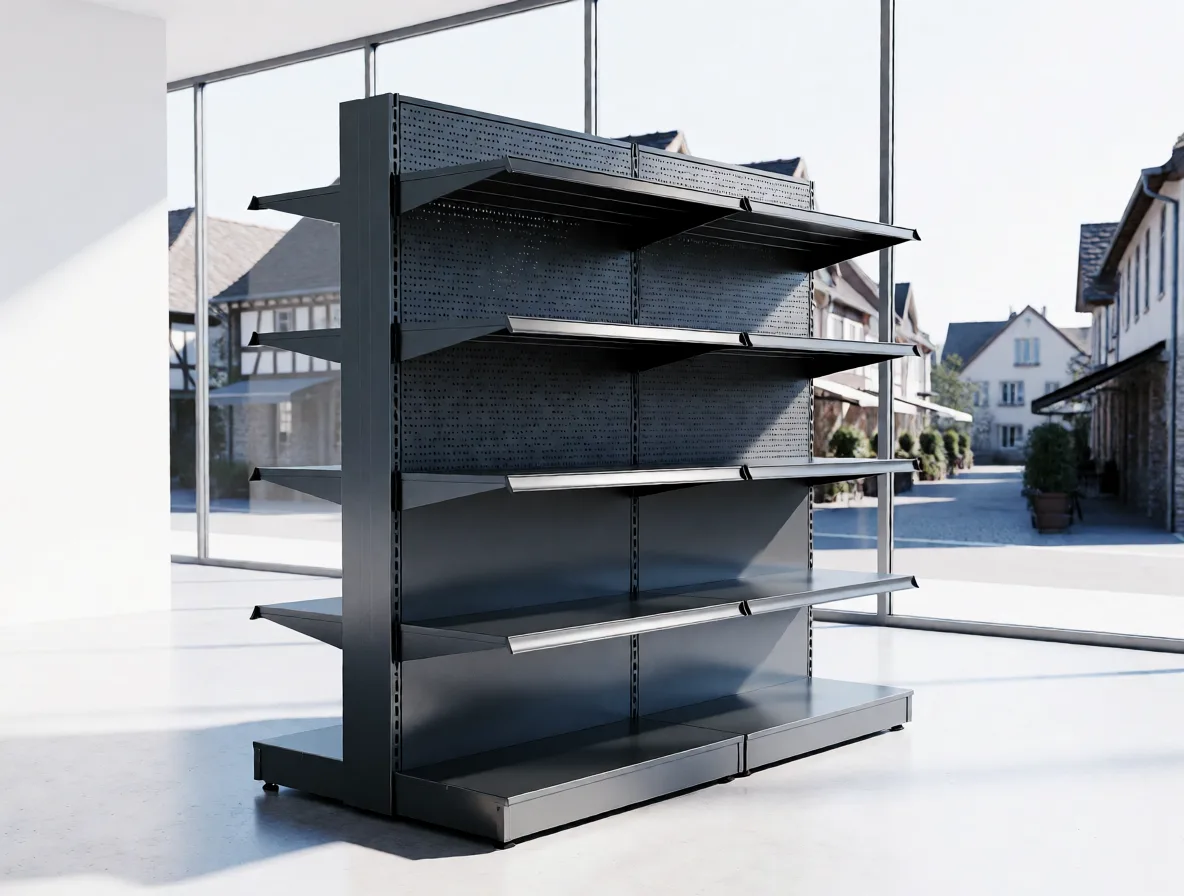
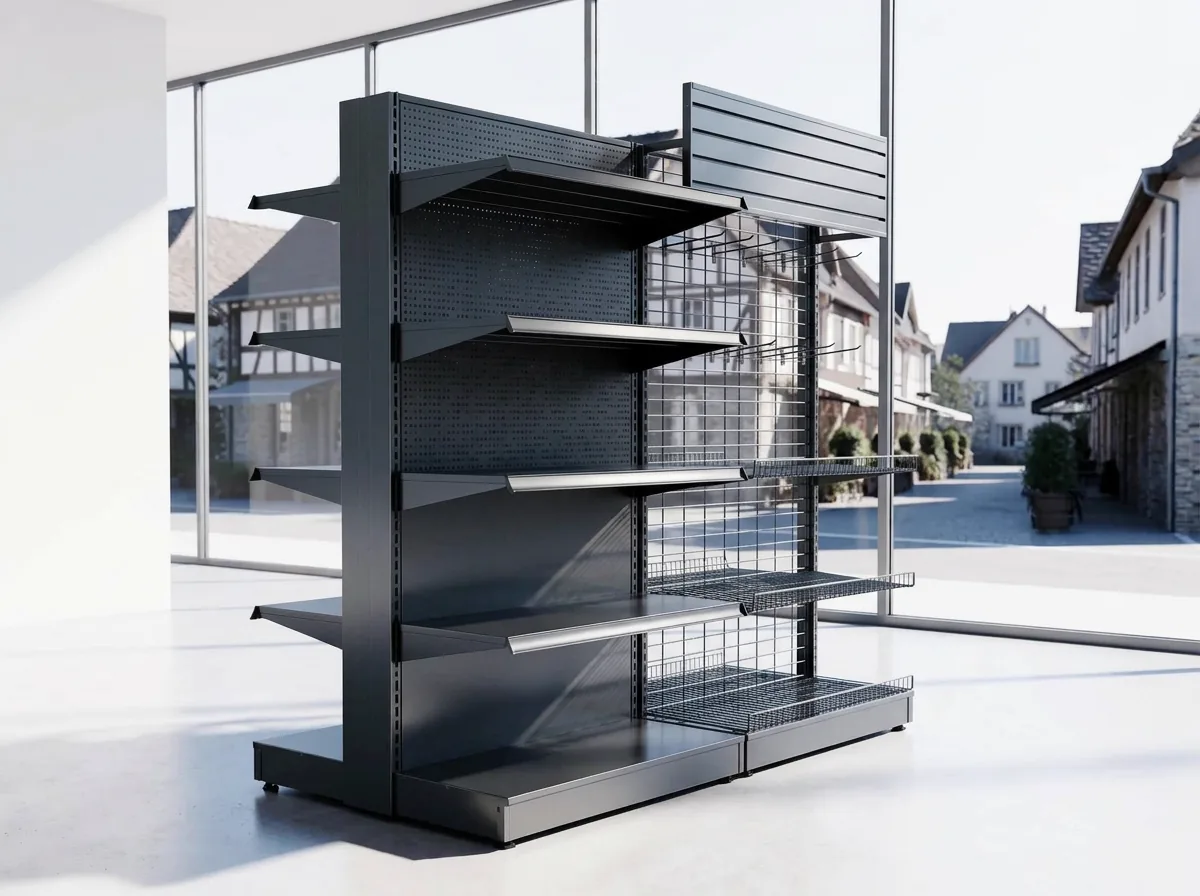
Gondola uprights, shelves, back panels and refrigeration carcasses — pressed, folded, welded, coated and packed at volume, to your drawing, in your finish.
You sell the system. We make the steel in it.
You sell the system. Your customer is the chain that buys it. We are the factory behind you.
Same tooling, same jig, same coating line, run after run — so shelf number four thousand will match shelf number one.
Three build envelopes
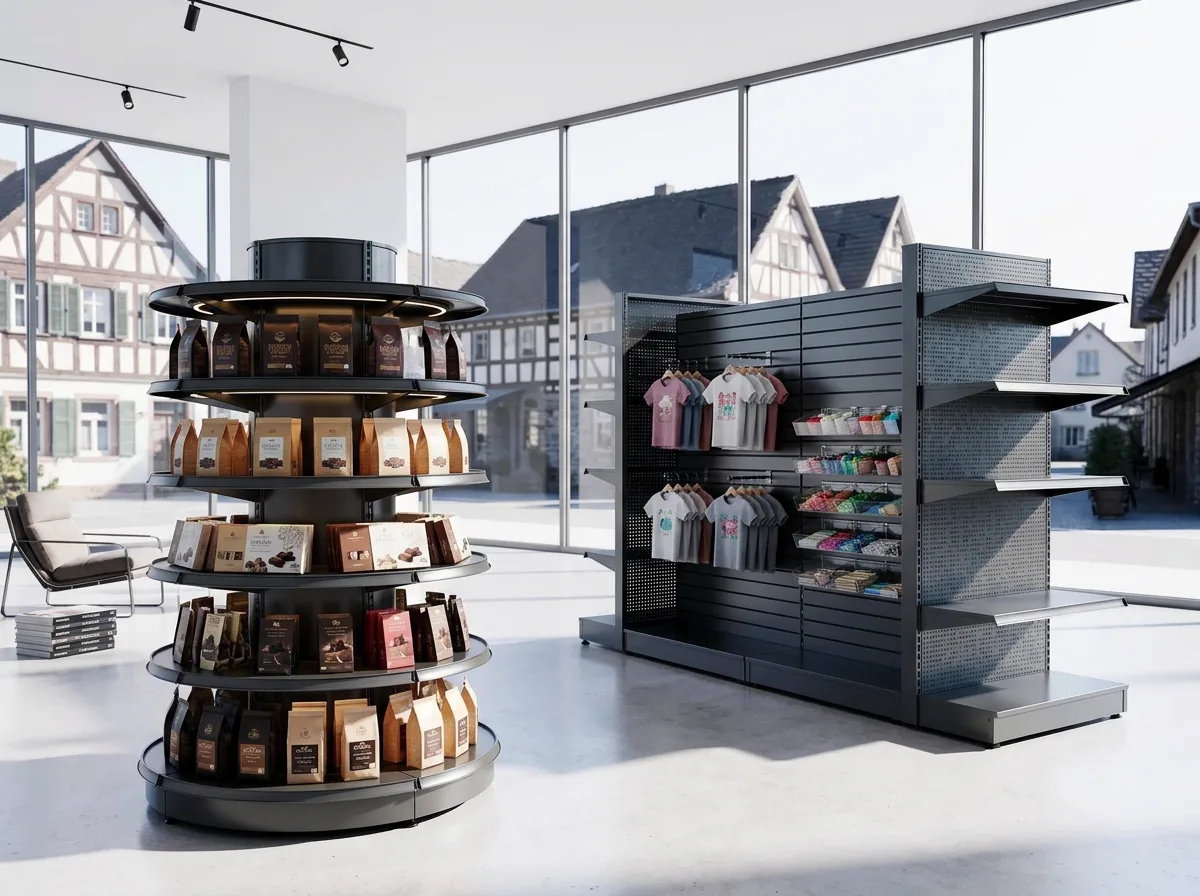
Build envelopes · 3Wall bay
perimeter runs, back panels, single-sided.
Island gondola
double-sided, higher load path, the volume workhorse.
Chilled carcass
the fabricated body, door frame and finish for refrigerated display.
These are envelopes, not products. You draw the system; we tool for it.
How your drawing becomes a repeatable part
4 steps- quote1Estimate
You send the drawing. We estimate what it takes to build it.
Tooling costed as its own line, so you see what the changeover buys — not a piece price with the setup cost buried inside it.
- 6–8 weeks2Initial Sample
We integrate your part into our production system.
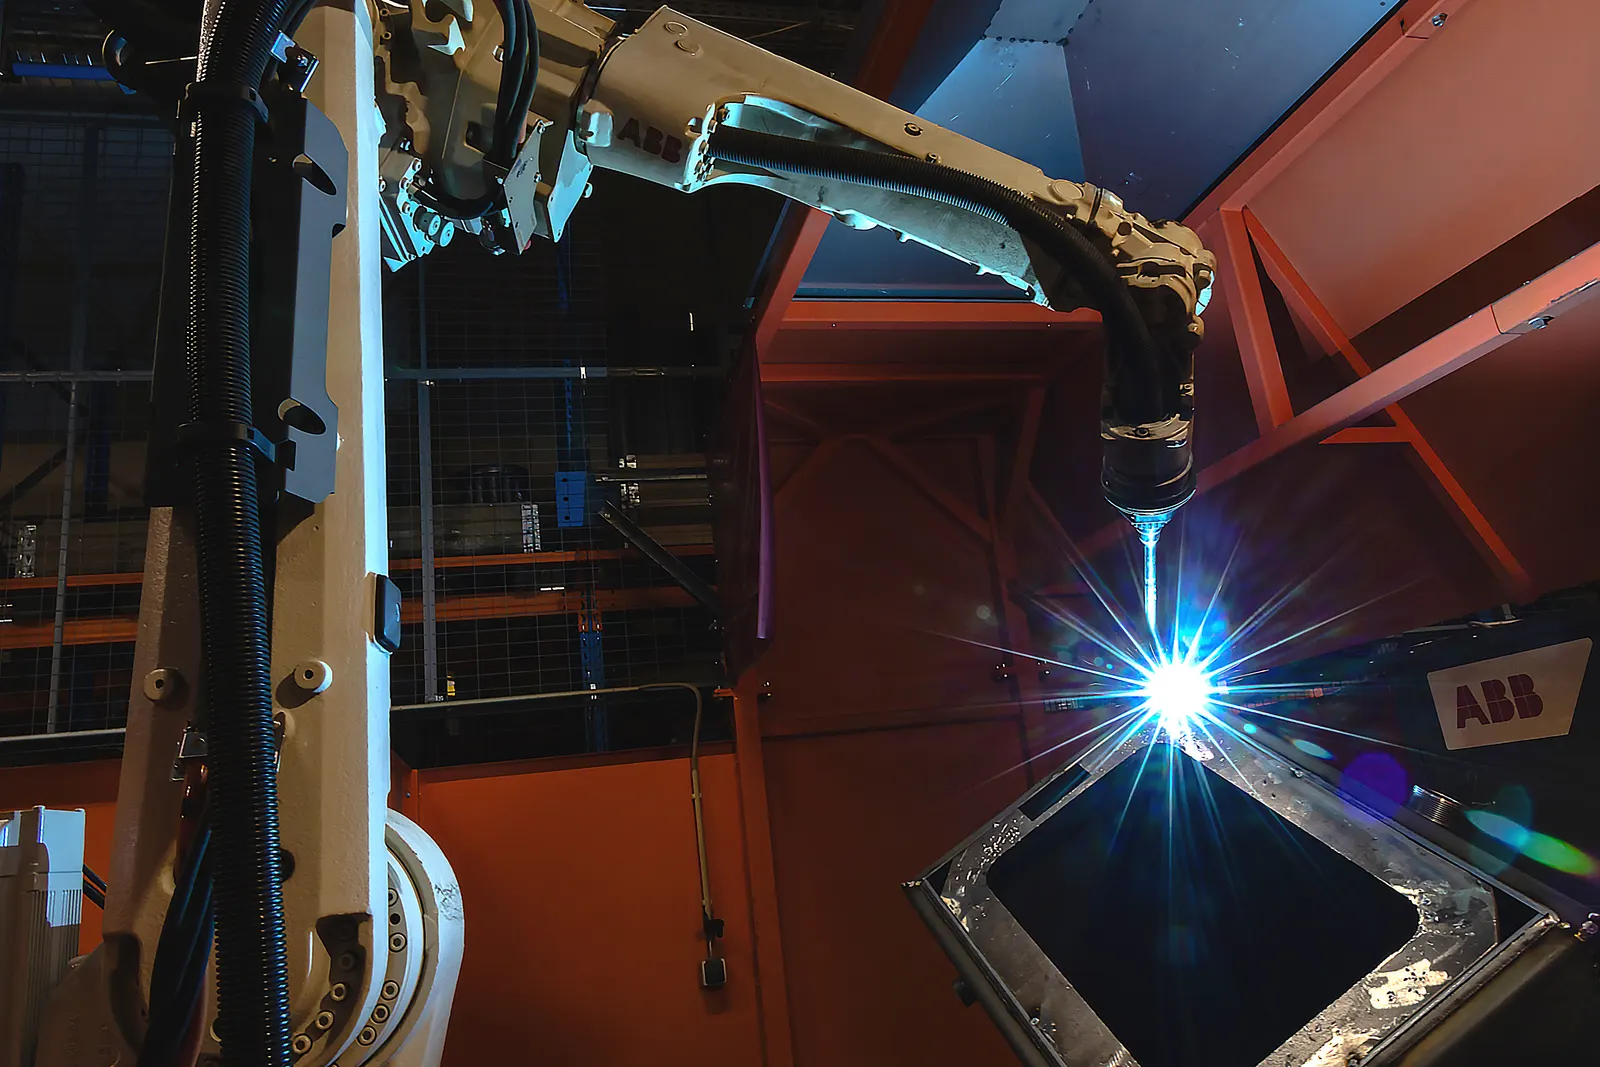
Production documentation, tooling, fixtures, the CAD/CAM programs that drive the cut, the bend, the weld — built once, so every unit after the first runs from the same file. If a process change would cut cost without touching form, fit or function, we flag it here. You decide.
- measurement report3Validation
We validate the first article — not just build it.
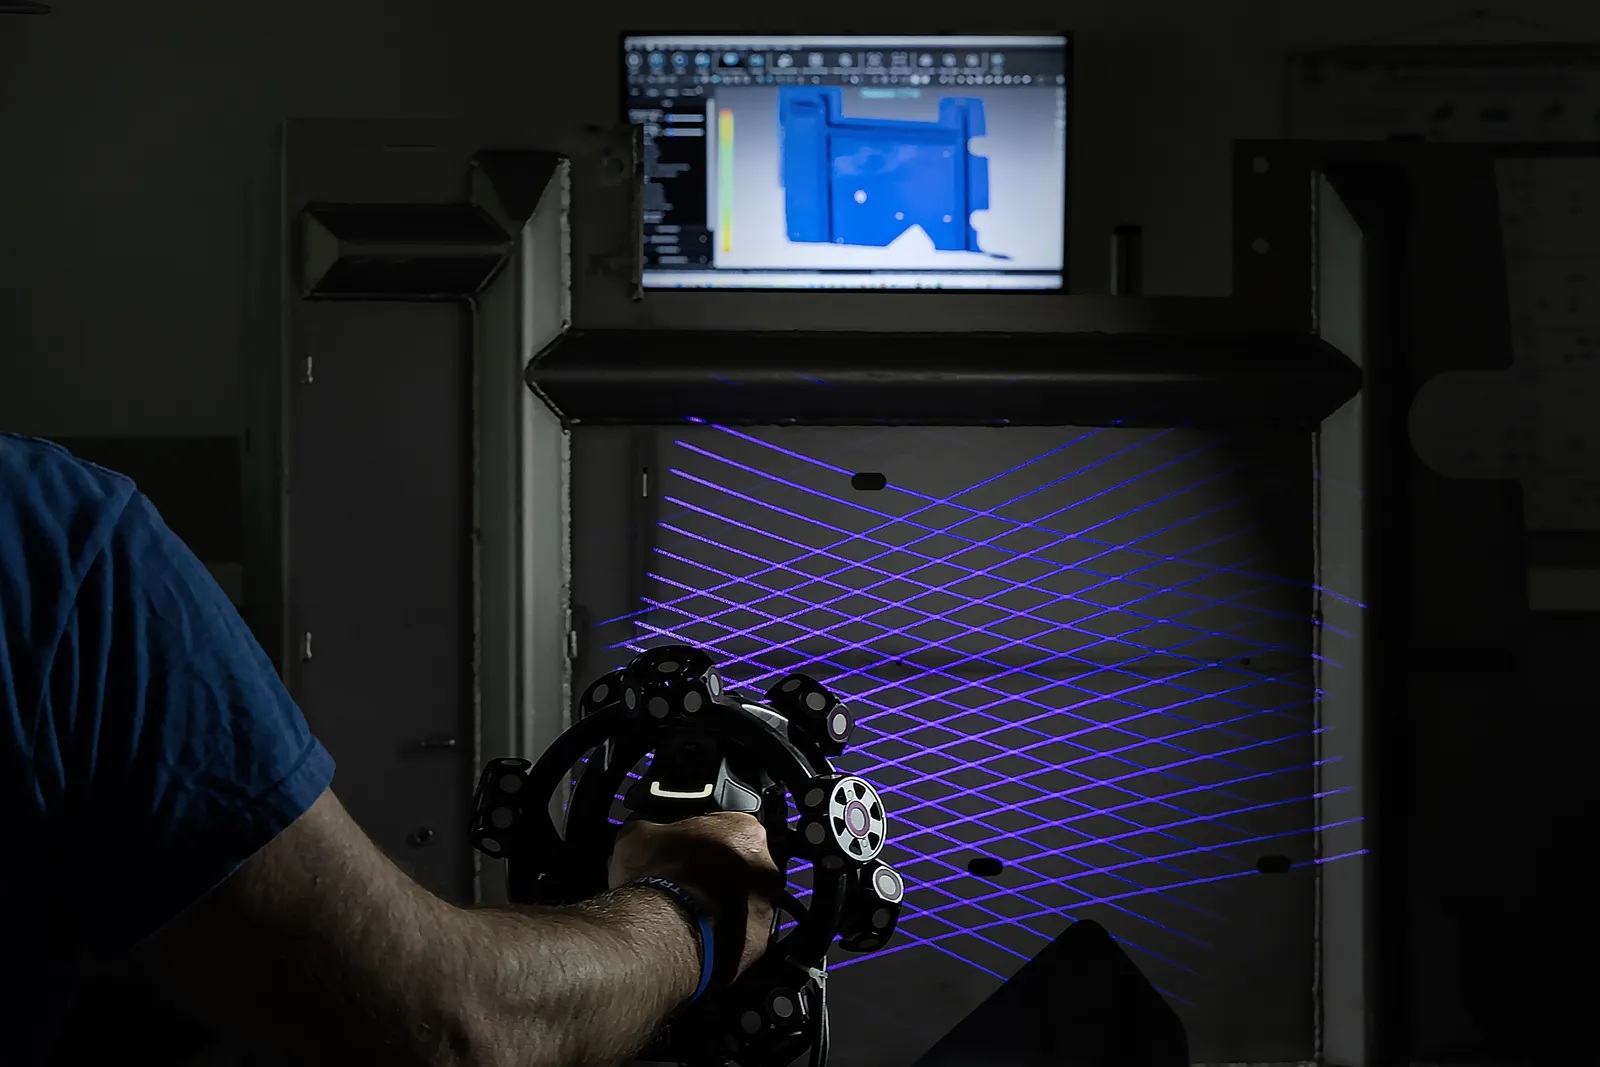
The first article is measured against your drawing, with a report attached. It either matches, or it doesn't, and you see which, before a single production run starts.
- 4 weeks from order4Manufacturing
Series production begins.
Four weeks from order. Minimum ten pieces. Minimum two hundred a year — the volume that keeps your tooling live and your part on our floor, not idle in a warehouse.
Build envelope
Sheet 1–15 mm| Sheet | 1–15 mm |
|---|---|
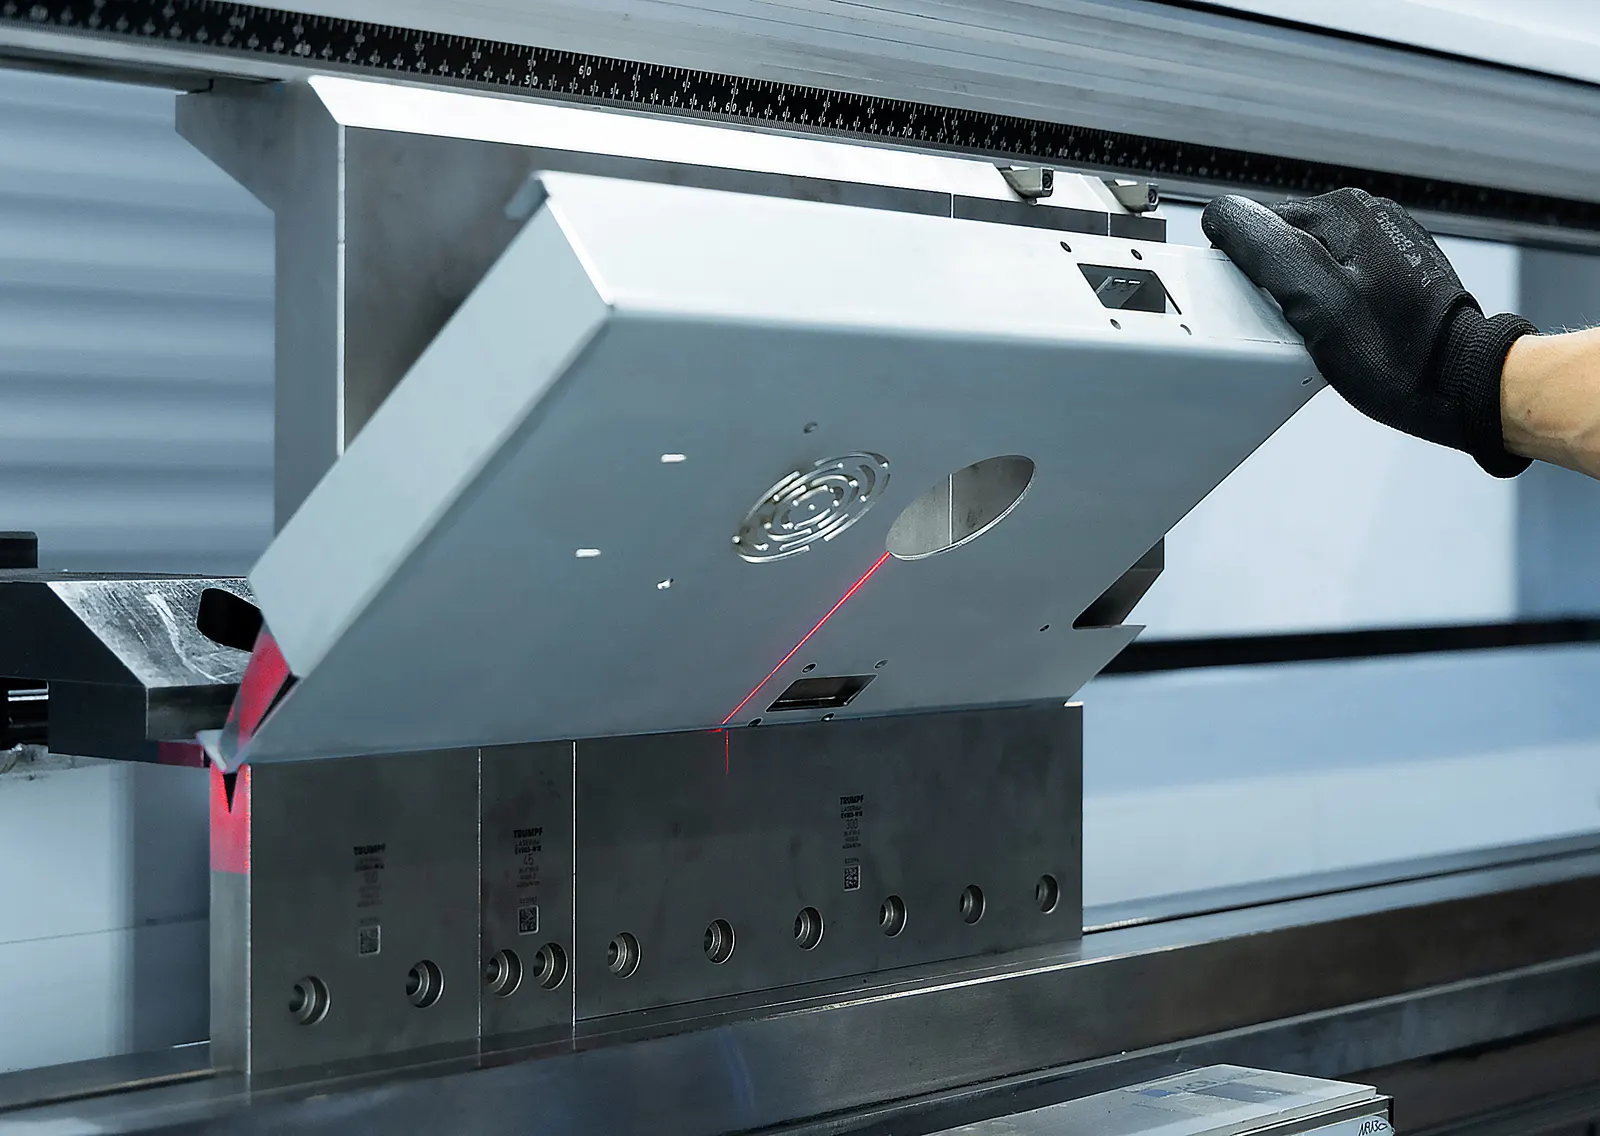
| Bending | CNC press brakes, 80–130 tons. Tooling radius 0.6–50 mm |
| Panel bending | enclosure parts up to 2.5 mm |
| Rolling | NC four-roll, cylindrical and curved |
| Materials | carbon steel and stainless (about 90%); aluminium (about 10%) |
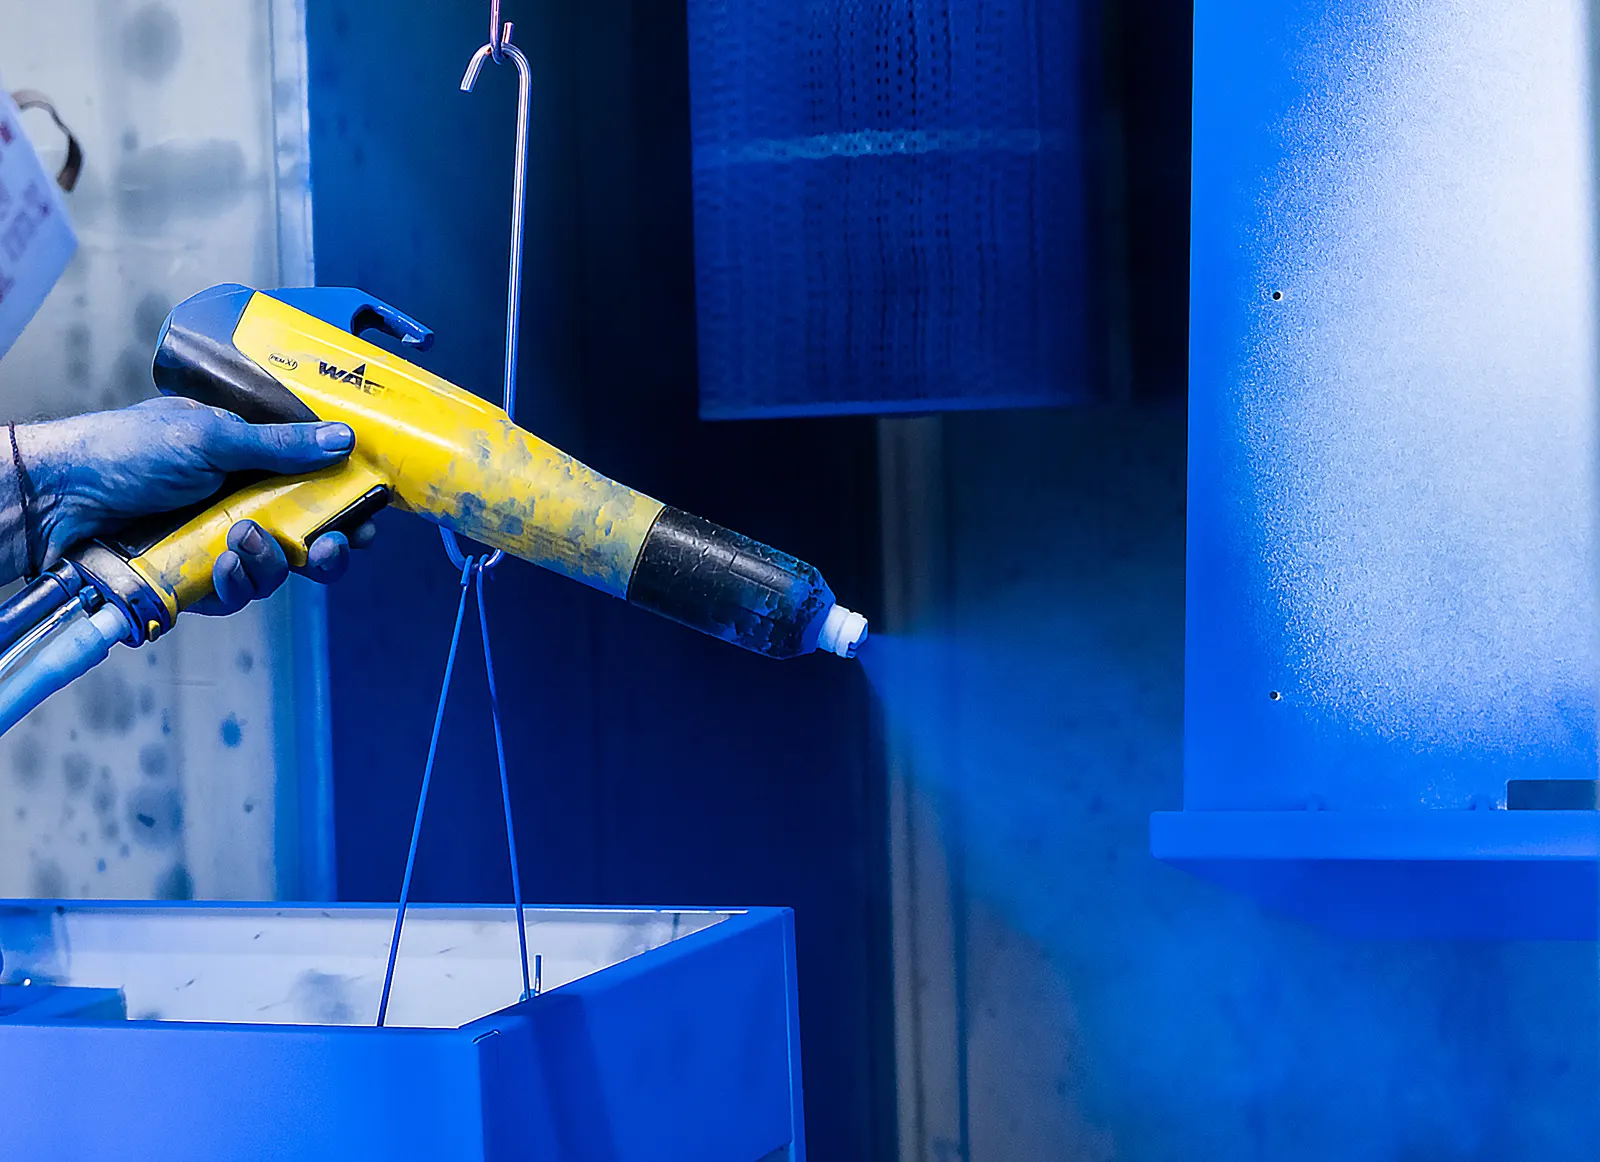
| Finish | powder coating in-house, any colour and texture. Galvanizing and KTL through certified partners |
| Series | 200–10,000 a year, from batches of ten |
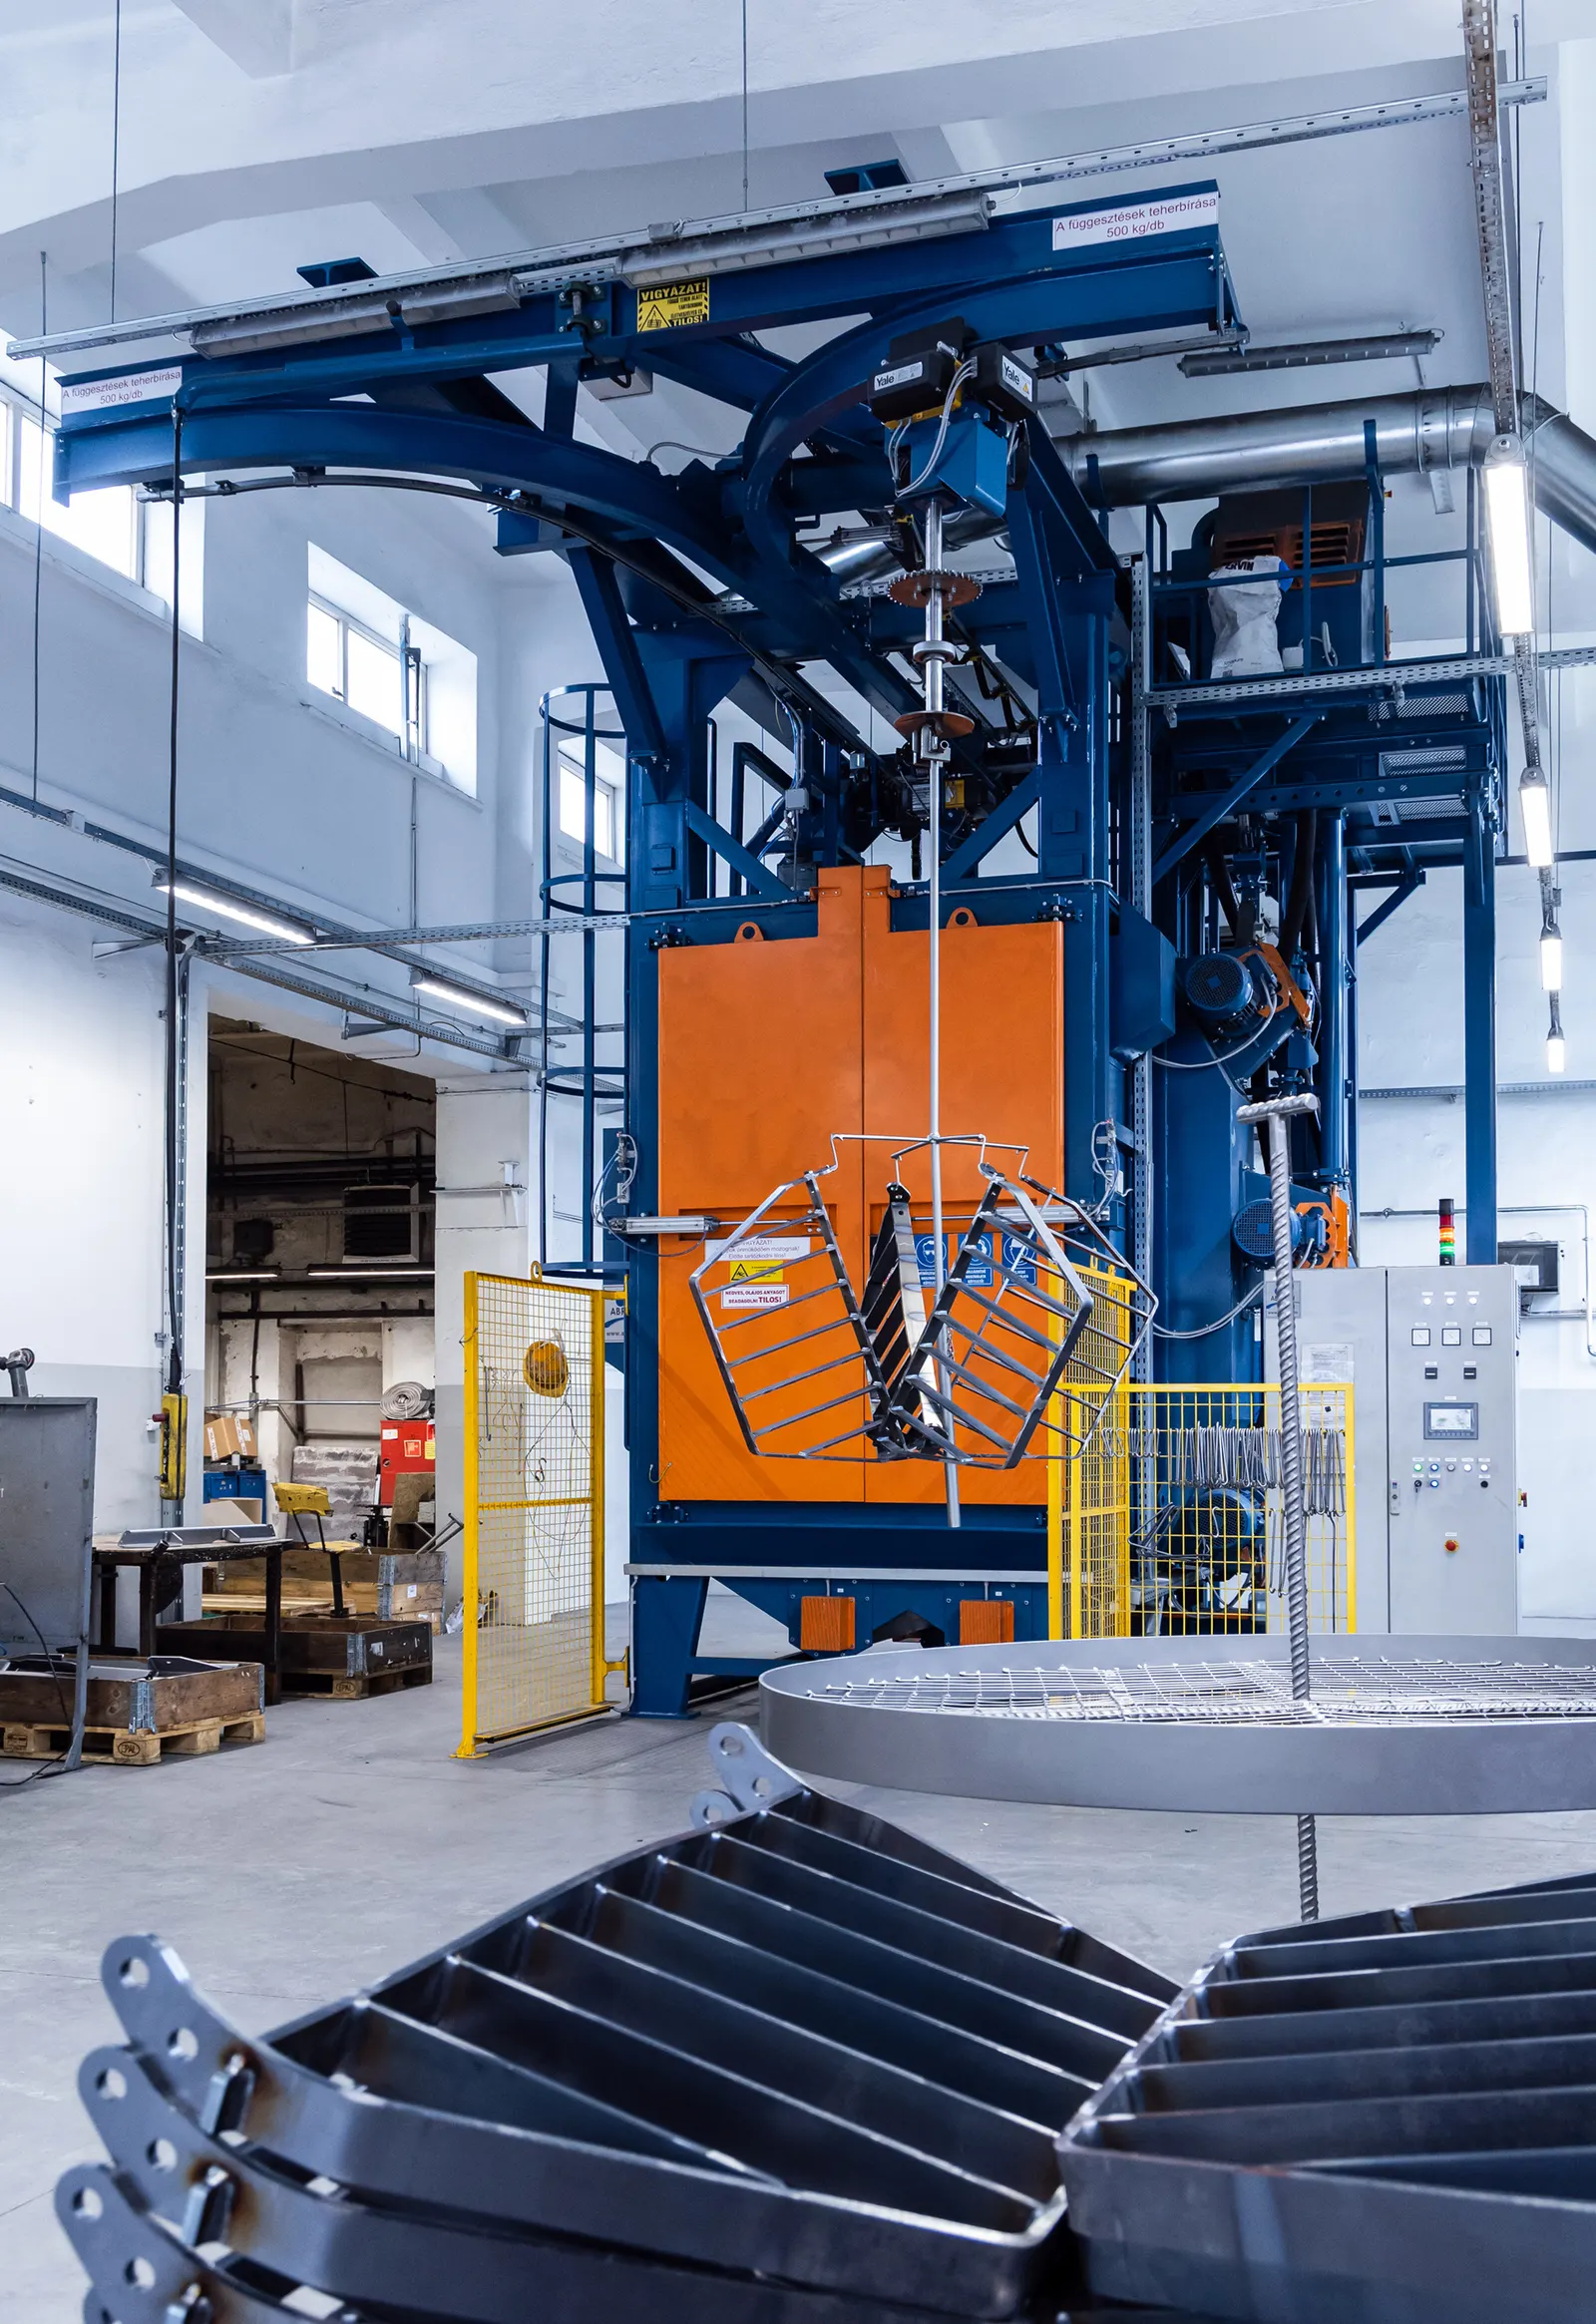
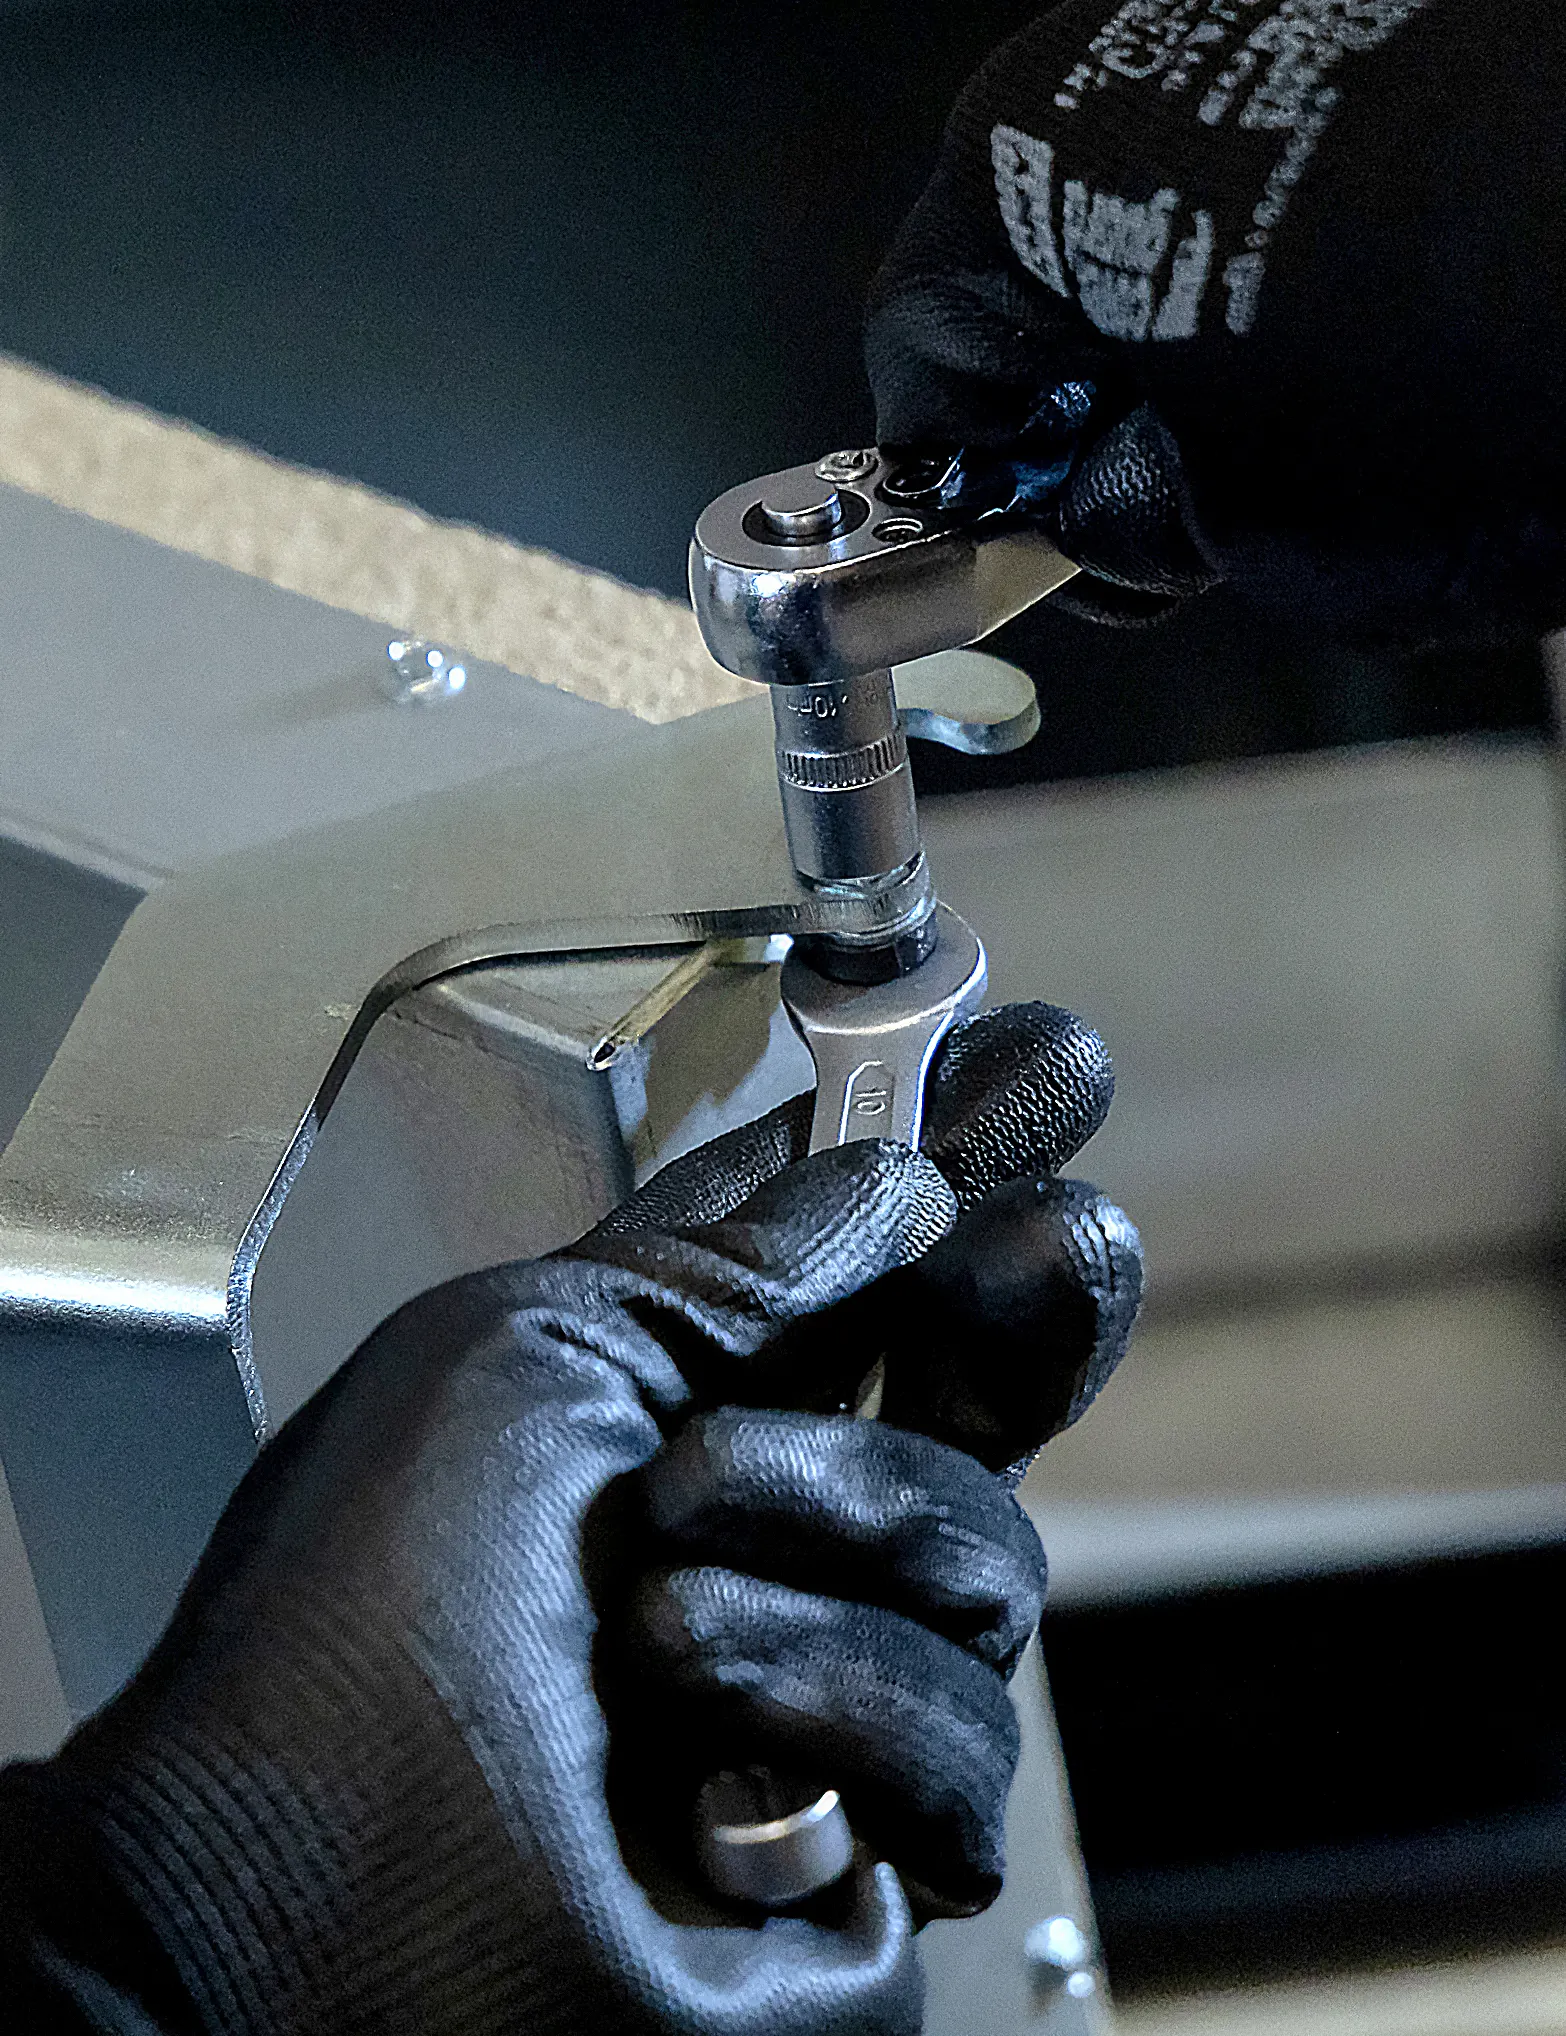
Cut → Bend → Weld → Blast → Coat → Assemble → Test
7 steps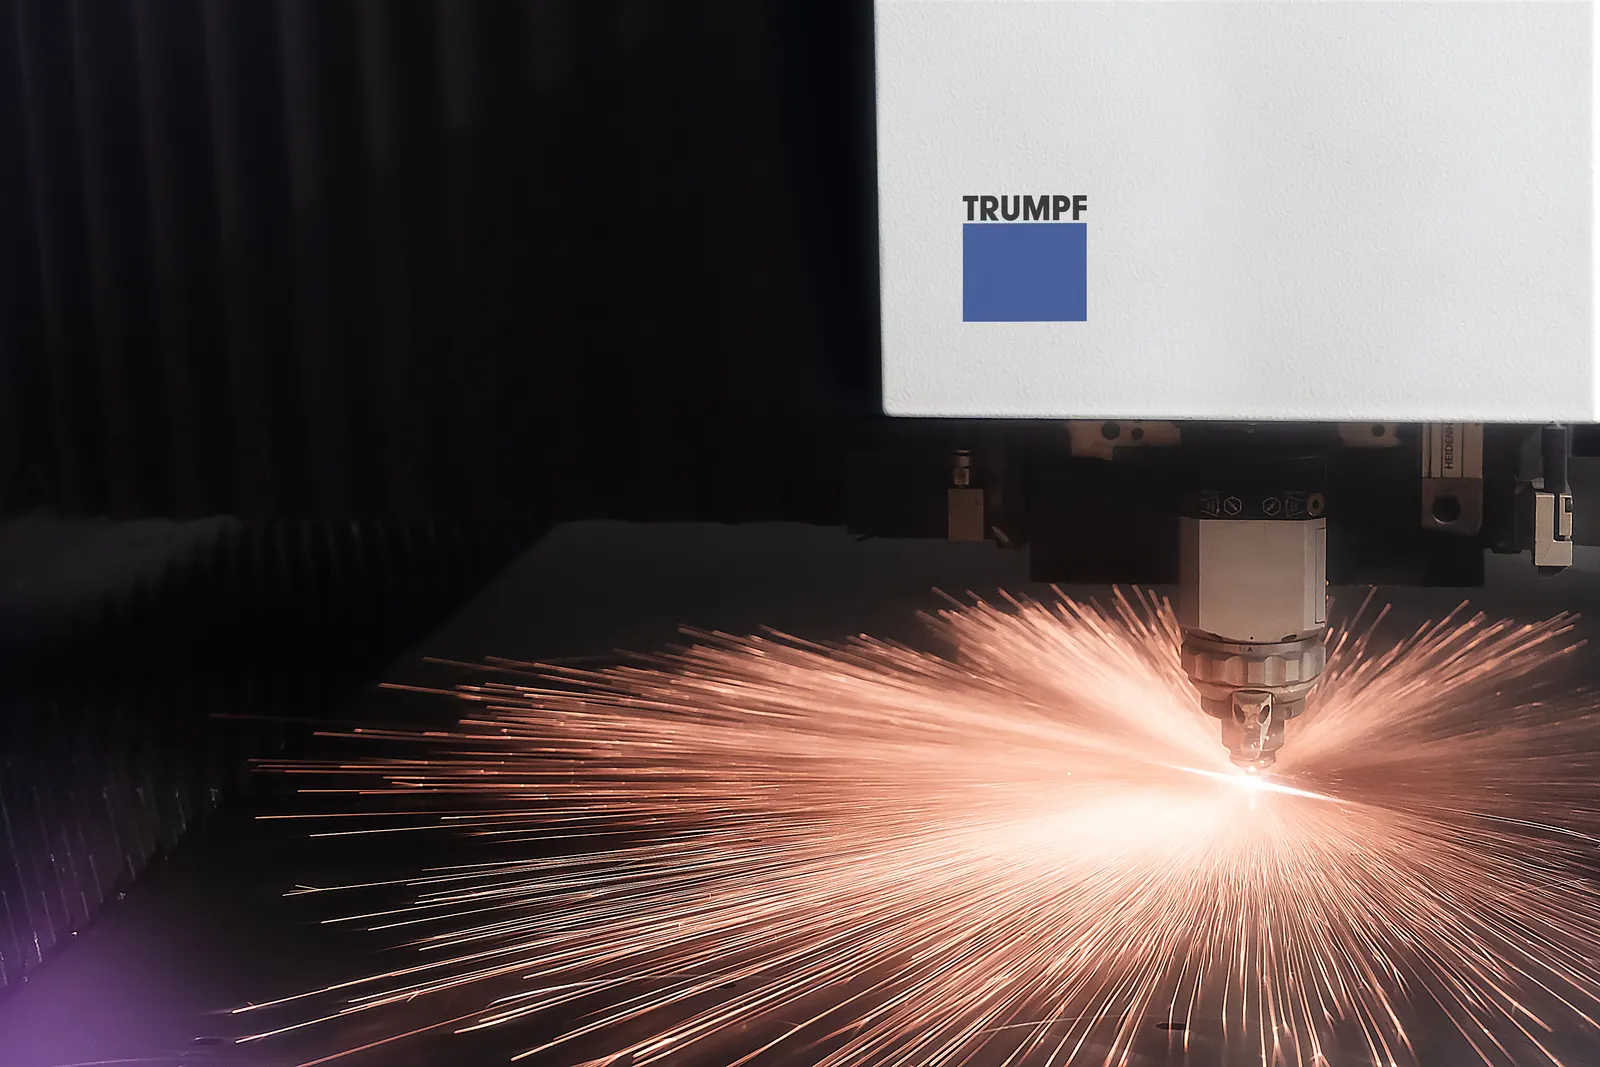
The hard part is not the first shelf. It is the four thousandth.
Batch consistency across a run nobody inspects one by one. Spare-part continuity years after the order closed, when a store needs one matching shelf and not a new system. And flat-pack packing that reaches site without a scratch on a surface the shopper will look at.
Tegometal, 50 mm, or your own — the pitch is a design decision and the design is yours. We build to your drawing. We do not impose a system on you.
We build the carcass, the door frame and the finish. The cooling pack integrates from your chosen supplier — we do not lock you to ours.
Series of 200 to 10,000 a year, from batches of ten. Four weeks from order. Flat-packed and palletised for shopfit logistics, shipped by truck into Western Europe.
Send us a drawing, or book 30 minutes.
One page, in the language you are reading. The same envelope, tolerances and numbers as this page — nothing extra to ask for.